 English
 中文简体


100%
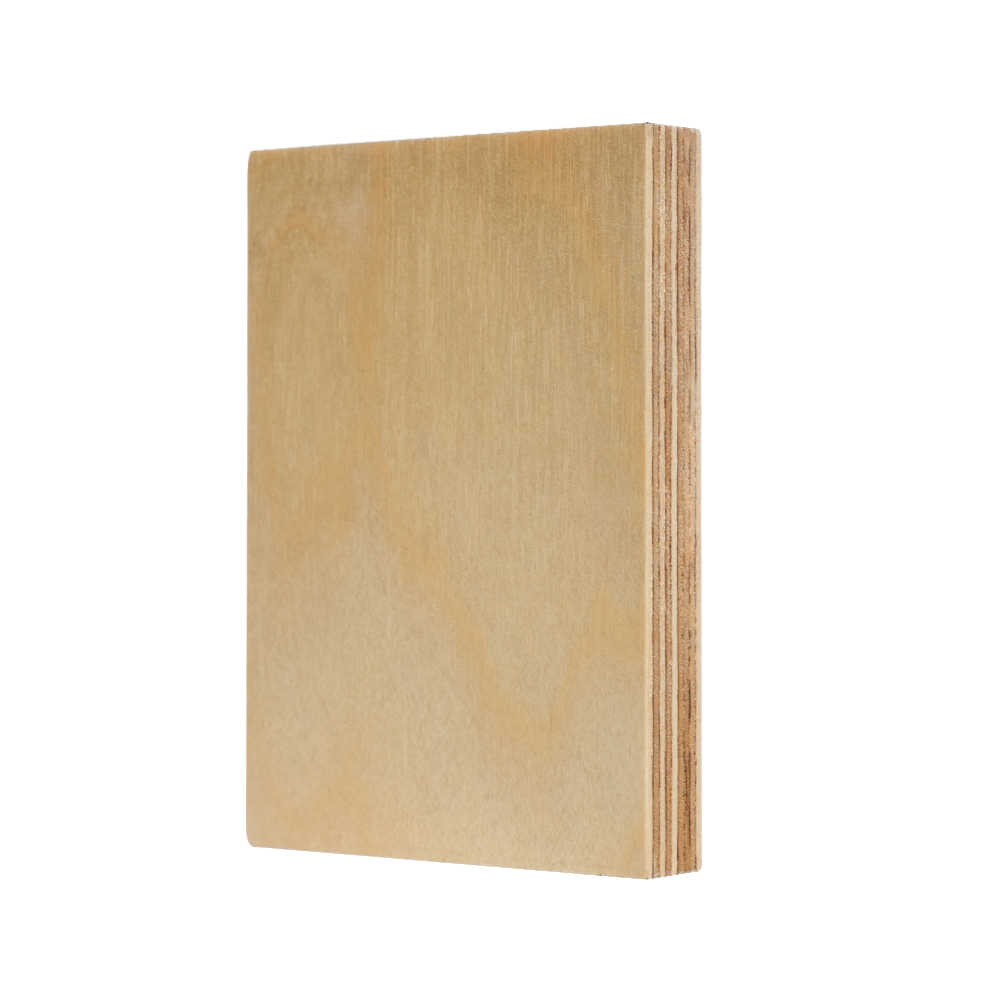
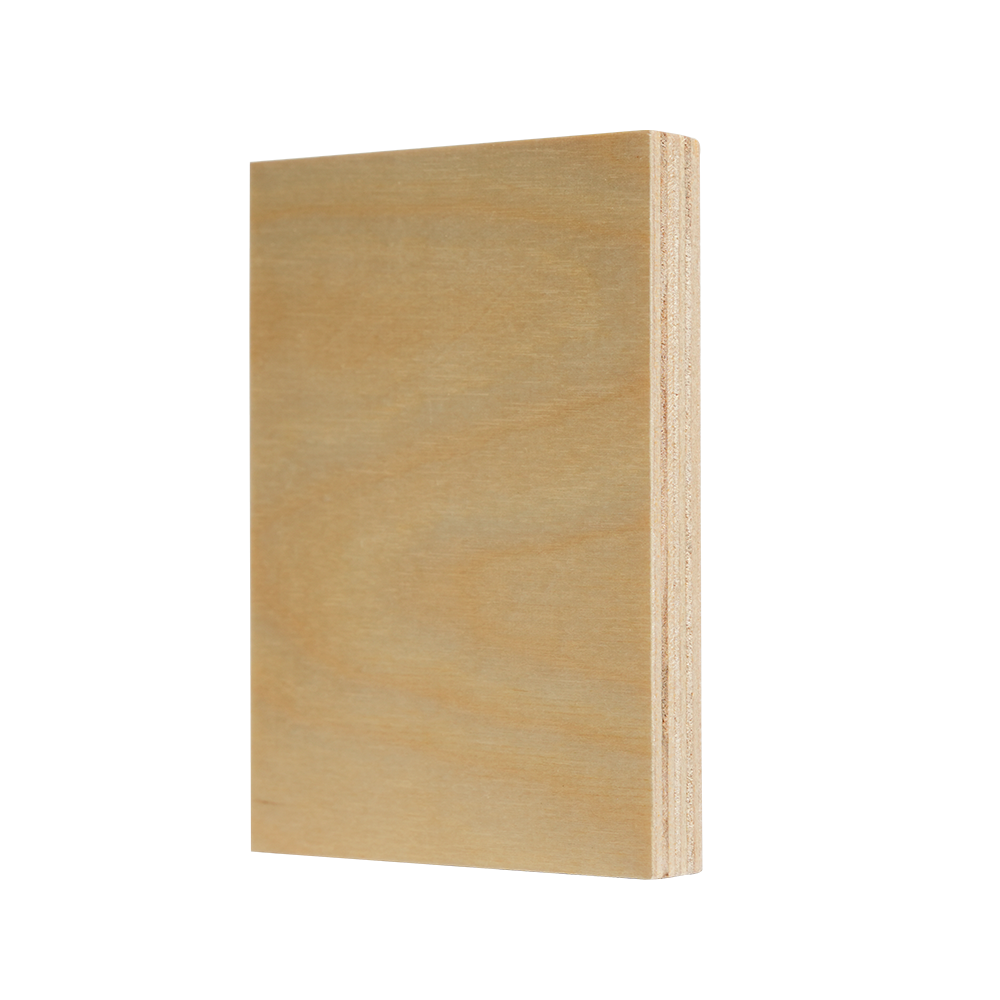
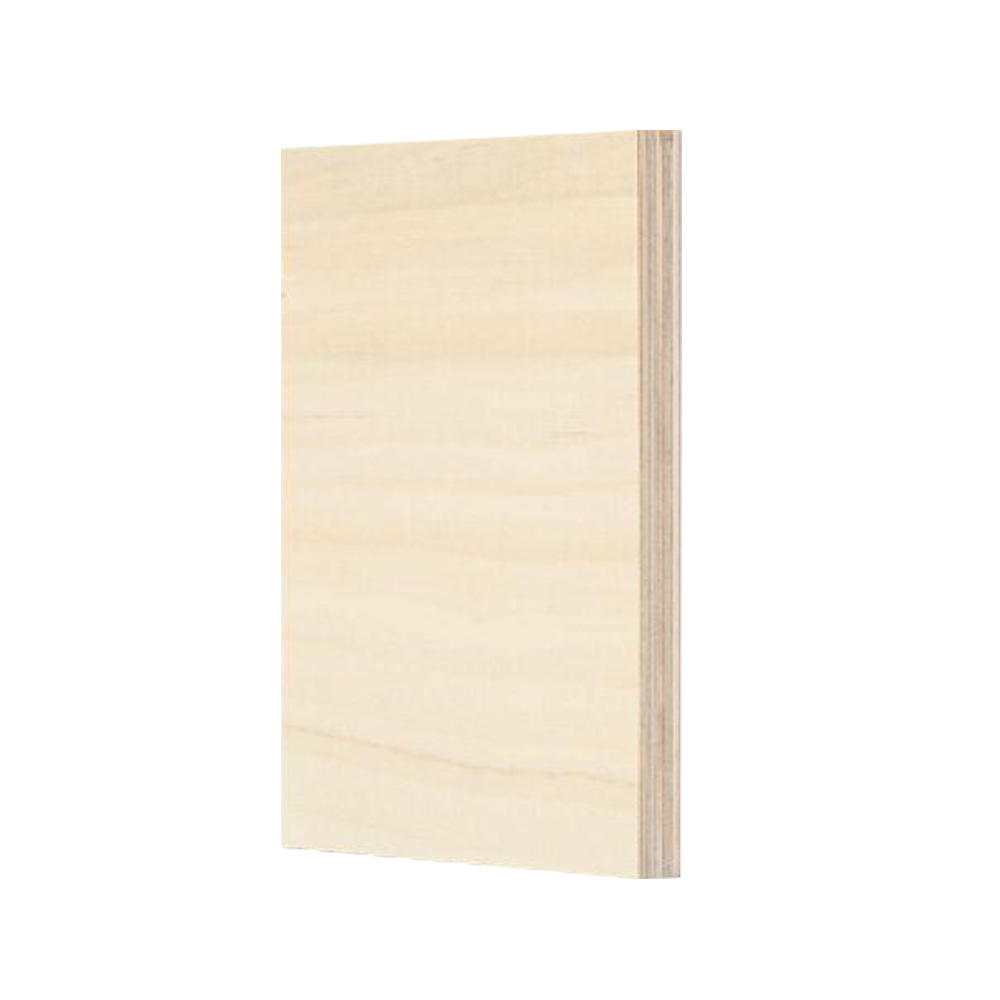
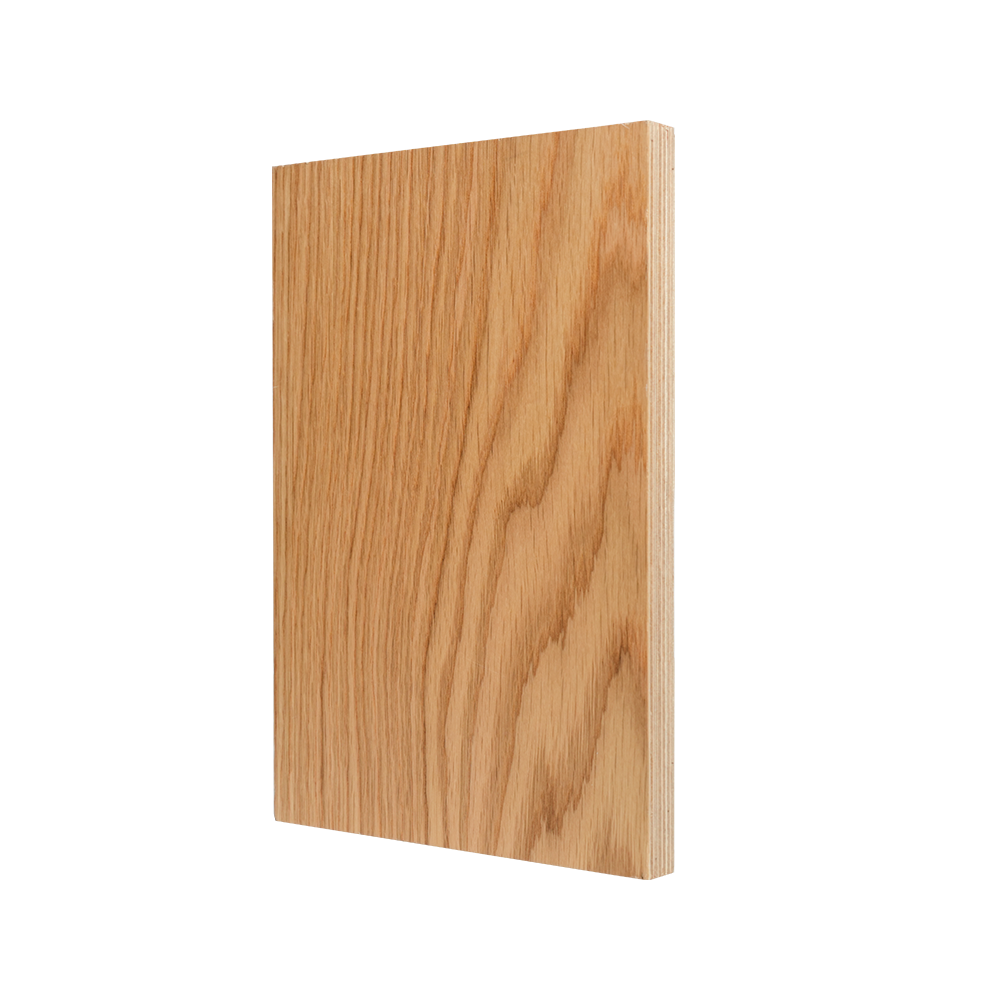
Birch plywood

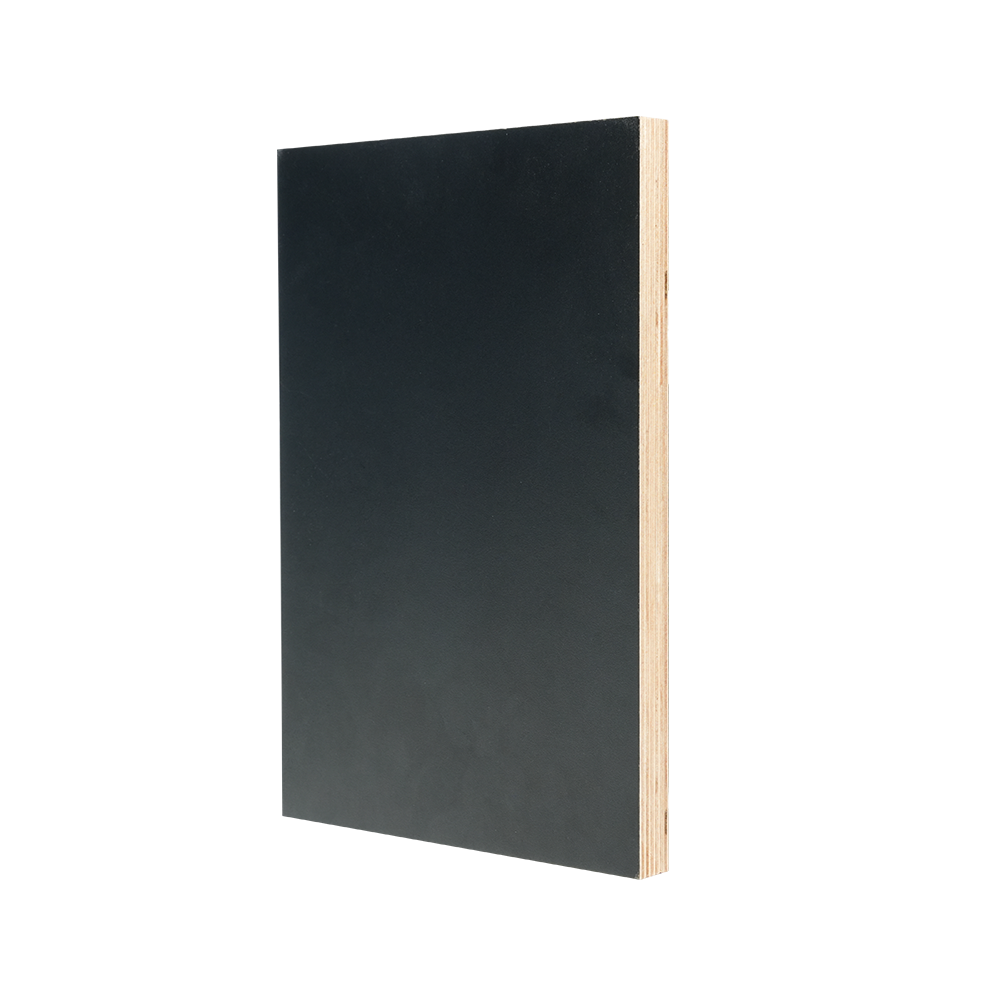
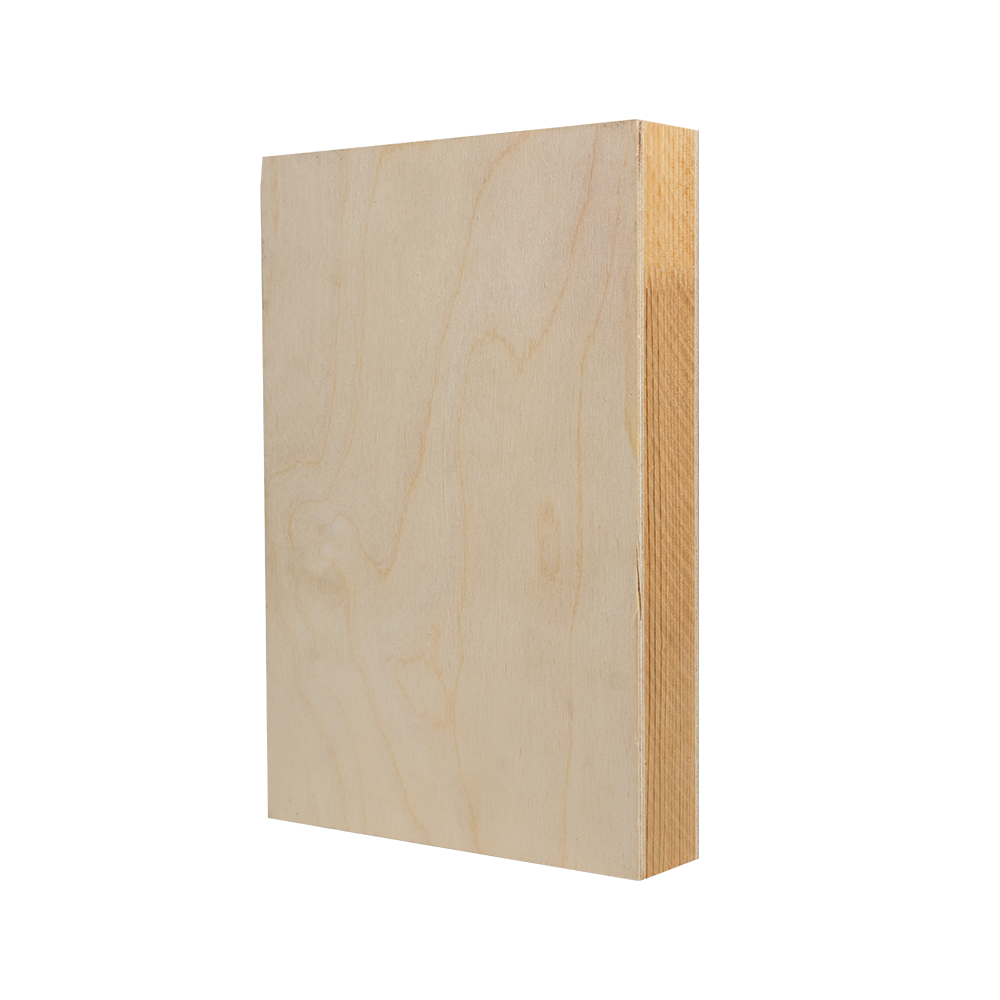
Container flooring is subjected to some of the harshest mechanical stress in the entire shipping industry — repeated forklift traffic, concentrated point loads from heavy cargo, and constant vibration during ocean transit. Container Flooring Birch Plywood Panels are engineered specifically to meet these demanding conditions, combining a dense, cross-laminated veneer structure with reinforced core layers that resist splitting under wheel loading. Unlike general-purpose plywood, container flooring panels must satisfy strict international shipping regulations, including CSC (International Convention for Safe Containers) compliance and IPPC fumigation marking requirements for wood packaging materials crossing international borders.
The manufacturing process for container-grade panels emphasizes uniform density distribution across the full sheet, minimizing the risk of localized weak points that could fail under a fully loaded forklift. Our panels typically feature a combi-core construction, integrating high-density hardwood layers with birch veneer facing to balance strength, weight, and cost-efficiency for large-volume container manufacturers. Every batch undergoes static and dynamic load testing to verify it meets the flooring specifications required by major container leasing companies and shipbuilders across Asia, Europe, and North America.
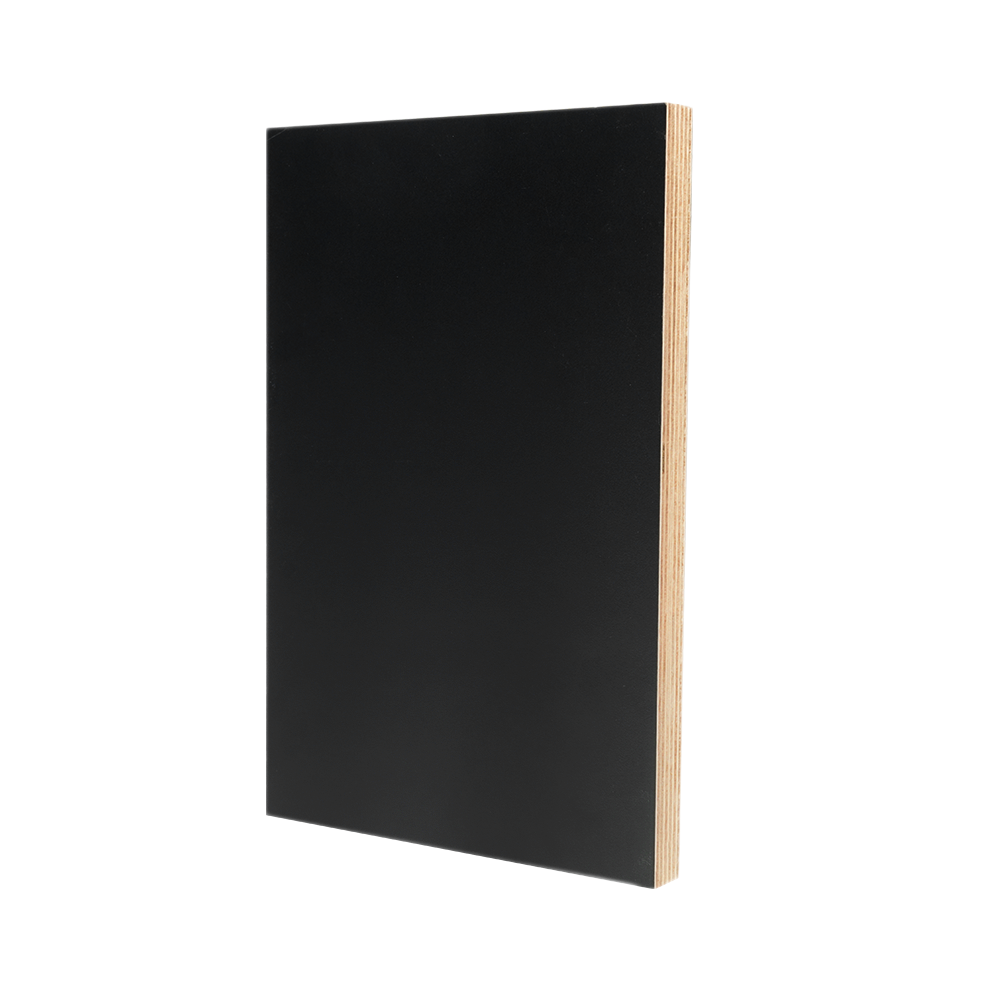
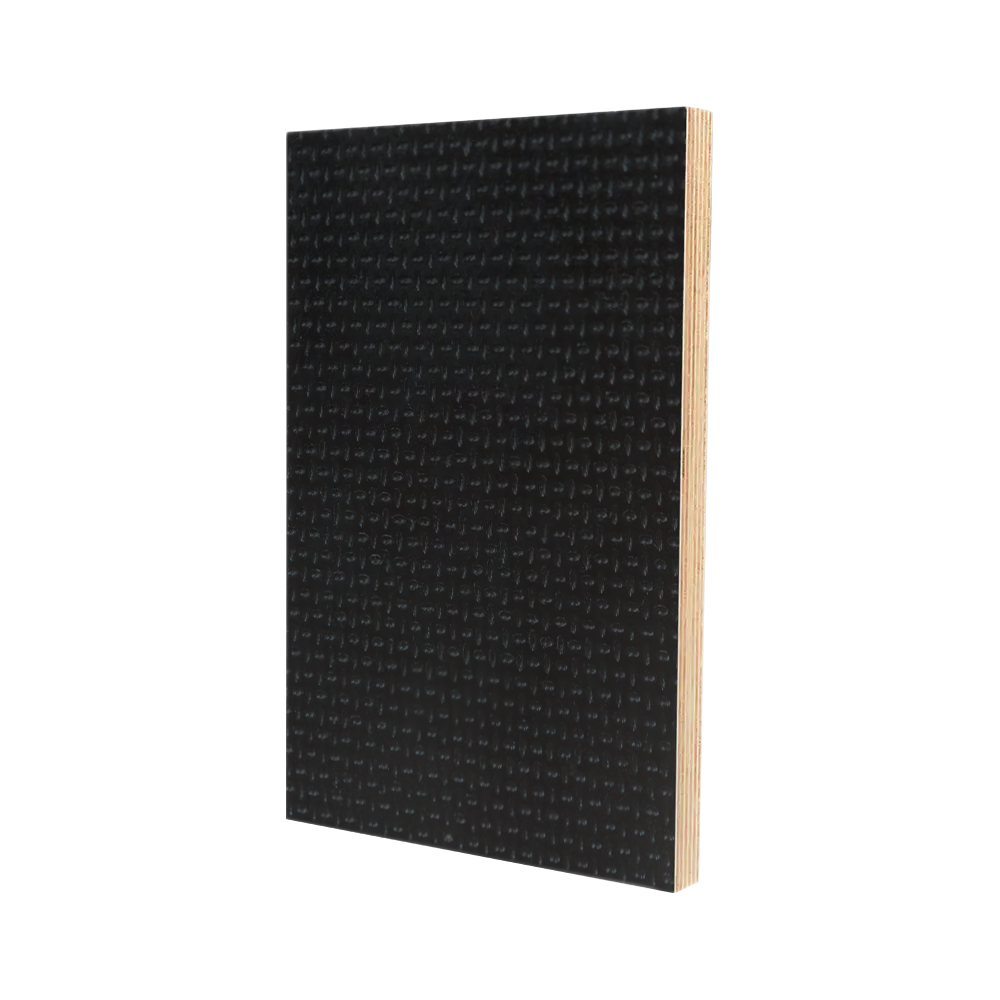
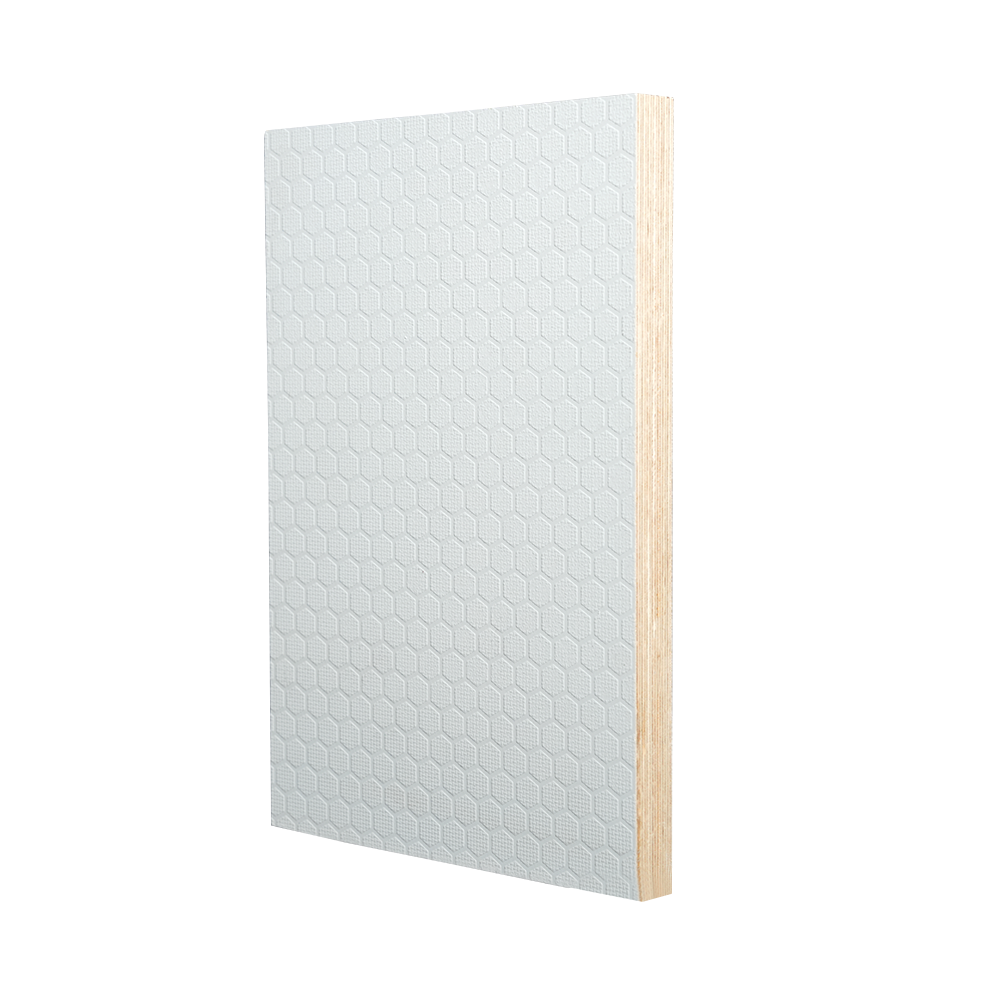
Surface treatment is equally critical. Container flooring panels are typically finished with a phenolic-impregnated film or an anti-slip coating to protect against moisture ingress from condensation inside sealed containers, while providing sufficient friction for safe cargo handling. This waterproof surface layer also protects against spillage from various cargo types, extending the operational lifespan of the container floor well beyond a standard 10 to 15-year service cycle, reducing total cost of ownership for fleets.
As global logistics infrastructure expands, demand continues to grow for container flooring solutions that balance structural performance with responsible sourcing. Our flooring panels are produced from sustainably harvested logs and bonded with WBP phenolic adhesive systems that maintain full integrity even in the fluctuating humidity and temperature conditions experienced during transoceanic shipping routes, from tropical ports to sub-zero winter transit corridors.
| Core Material | Combi Core (Birch + Hardwood) |
| Face/Back Grade | BB/CC, Container Grade |
| Standard Thickness | 15mm to 30mm |
| Panel Dimensions | 1160x2280mm / 1220x2440mm |
| Glue Type | WBP Phenolic (100% Waterproof) |
| Moisture Content | 8% - 12% |
| Density | 680kg - 750kg/m3 |
| MOQ | 1x20GP Container |
| Lead Time | 20-30 Days |
| Packaging | Fumigated Export Pallet Packing |
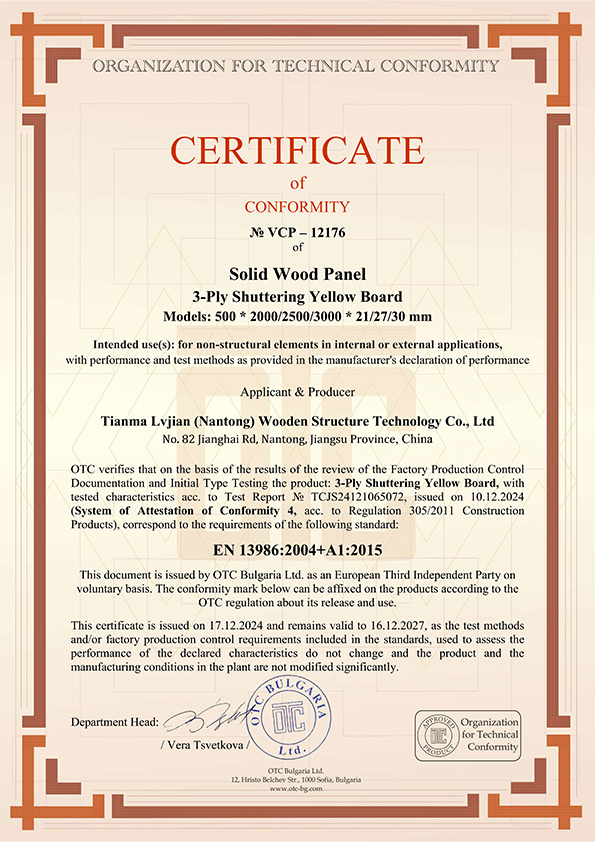
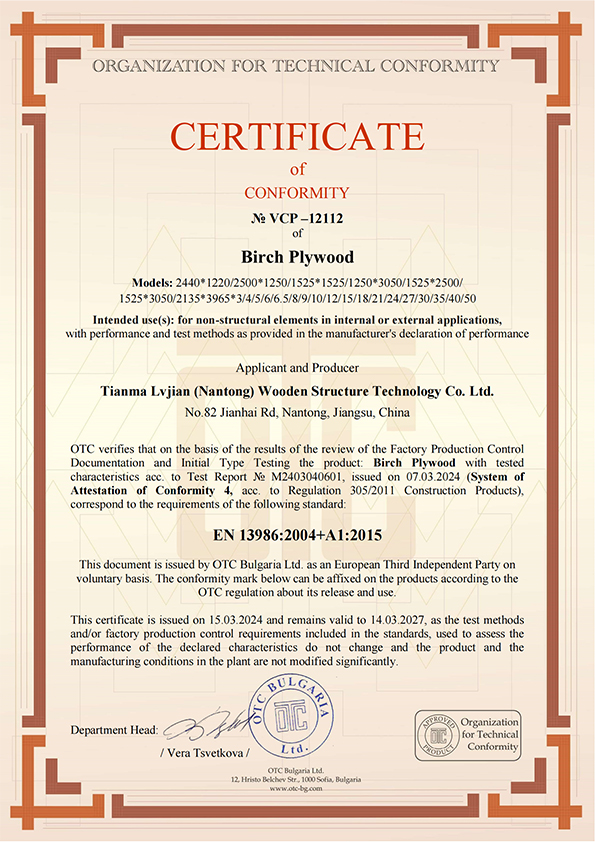
| Certifications | CSC, IPPC, ISO9001, CE |
| Raw Materials | Northern Birch and Hardwood Combi Core |
| Customization | Thickness, Surface Film Color, Panel Size |
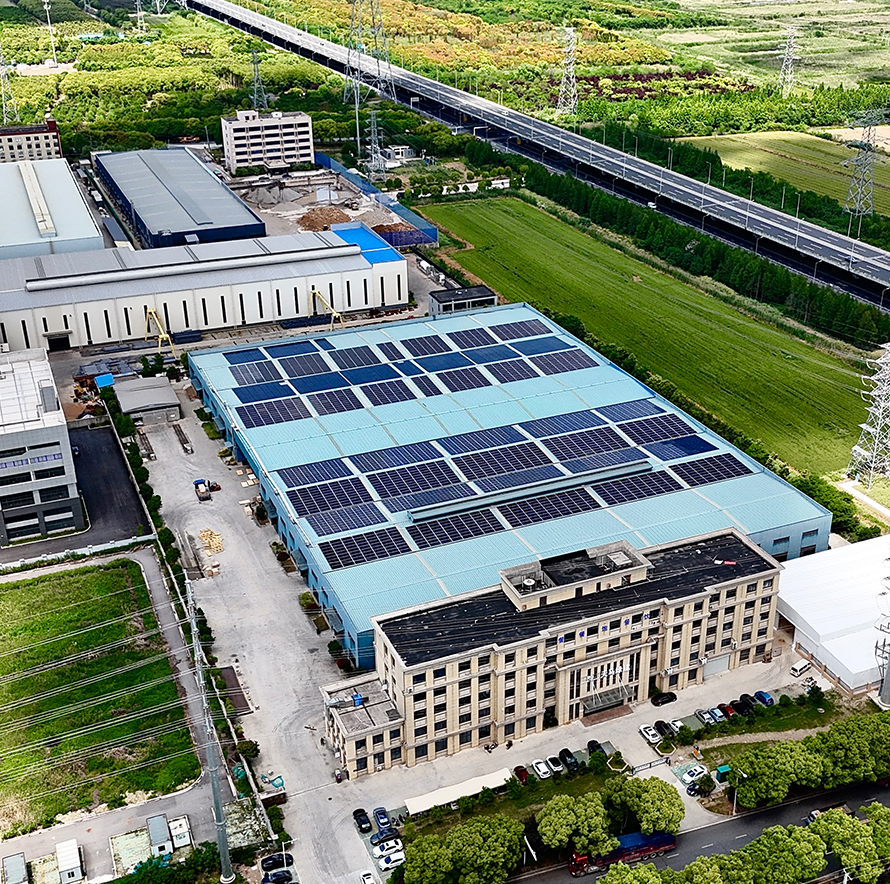
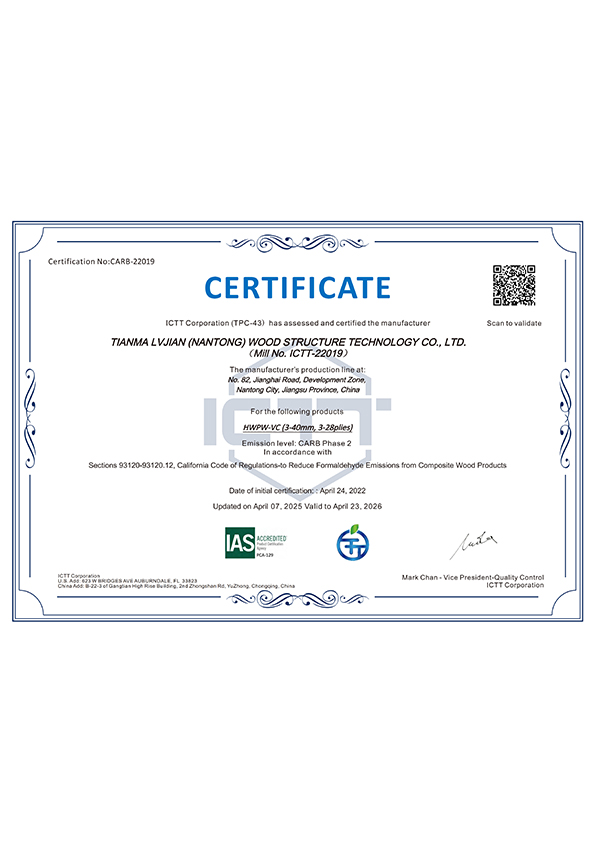
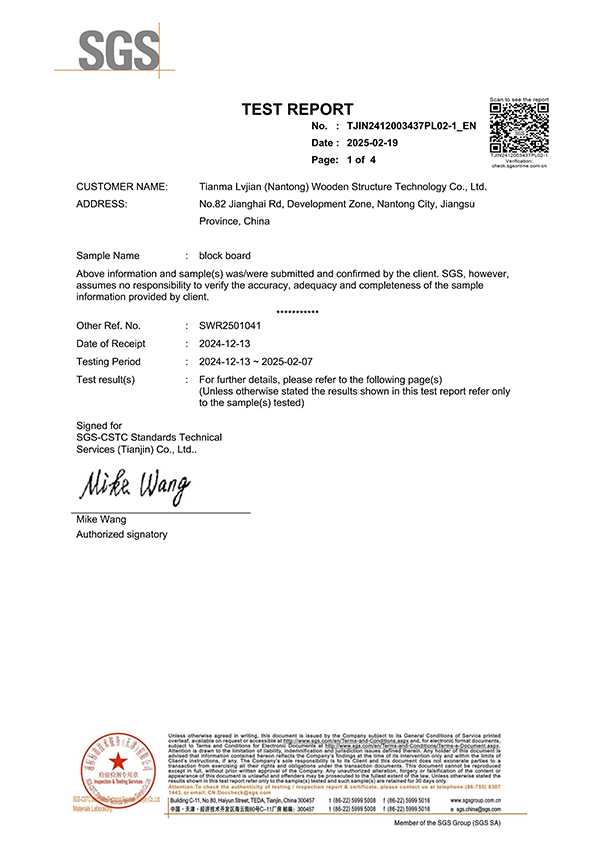
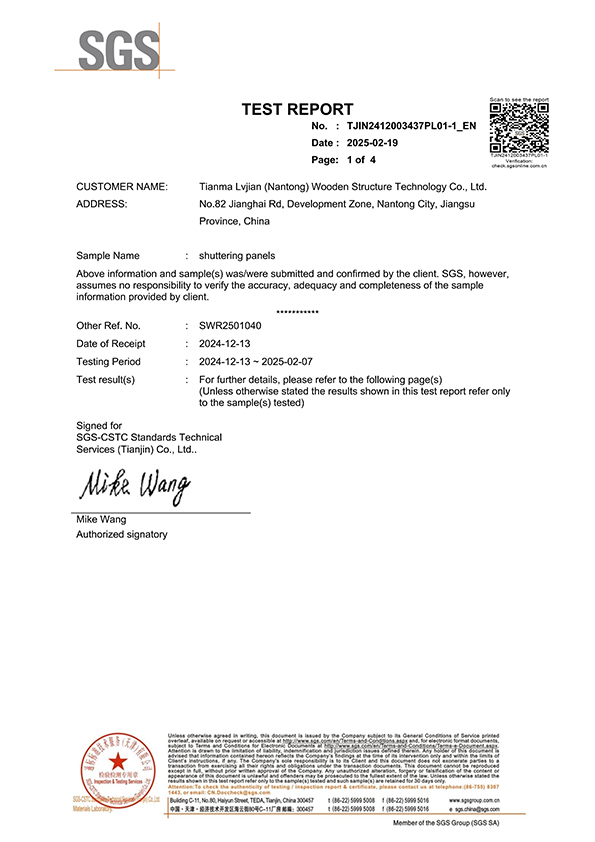
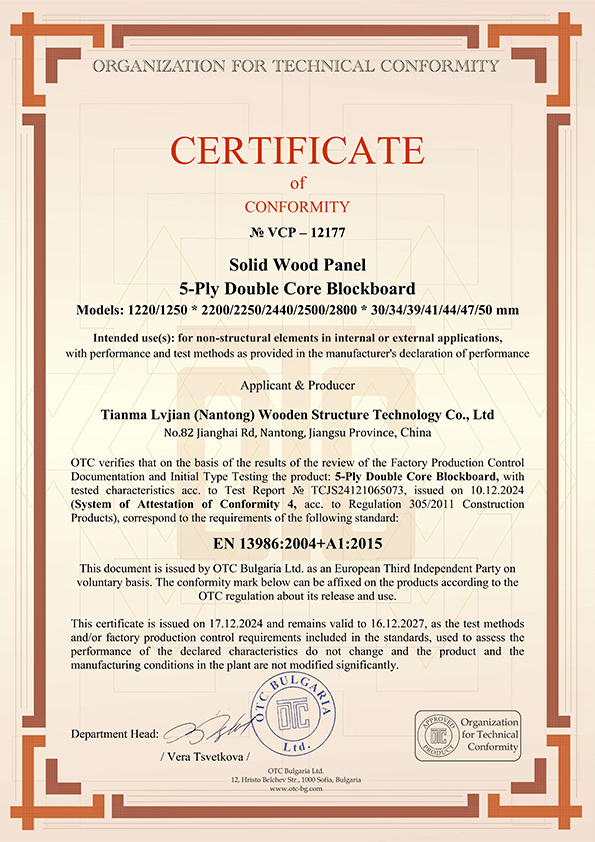
Given the specialized nature of container flooring, we coordinate closely with container manufacturing plants to align delivery schedules with production line requirements. Standard payment terms include 30% T/T deposit with balance against the bill of lading, along with L/C at sight for larger volume contracts. Panels are shipped through Lianyungang or Nantong port with fumigated pallet packaging that satisfies phytosanitary requirements in destination markets across the Americas, Europe, and Southeast Asia, minimizing the risk of customs delays.
Each container flooring panel is built from a combination of high-density hardwood core veneers reinforced with birch face and back layers, cross-laminated at alternating grain angles. This structural arrangement distributes concentrated loads — such as a fully loaded forklift wheel — across a wider surface area rather than a single point, which is the primary cause of premature flooring failure in lower-grade materials.
The phenolic film overlay bonded to the panel surface is heat-pressed under high pressure, creating a seamless waterproof barrier that also improves the coefficient of friction for safer cargo operations. This combination of internal engineering and surface protection allows our container flooring panels to consistently meet the demanding specifications set by major container manufacturers worldwide.
As container manufacturing scales to meet global trade demand, sourcing responsibly harvested timber has become a key differentiator for environmentally conscious logistics companies. Our container flooring panels are produced from birch and hardwood sourced through verified supply chains, with production processes designed to minimize waste through precision veneer peeling and panel layup. By selecting FSC-eligible raw materials wherever possible, we help container manufacturers align with increasingly strict environmental procurement policies across European and North American markets.
Get in touch with our team for quotes, technical specifications, and customized solutions.
Contact Us Now
Copyright © Tianma Lvjian Group Co., Ltd. Rights Reserved.
Wholesale Container Flooring Birch Plywood Panels Manufacturers